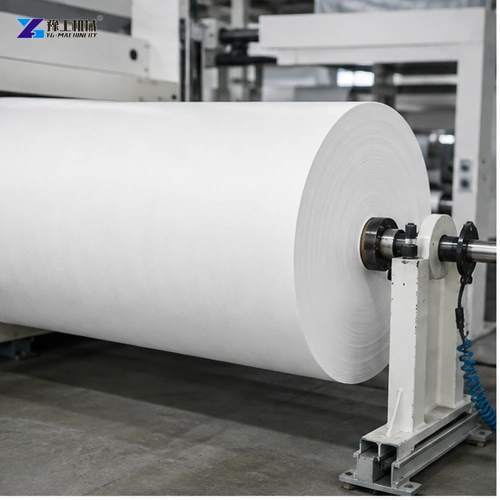
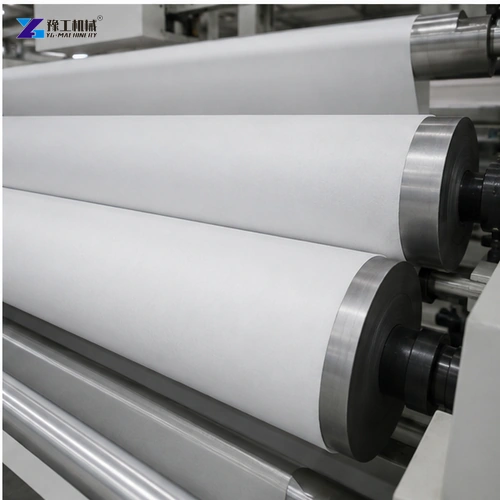
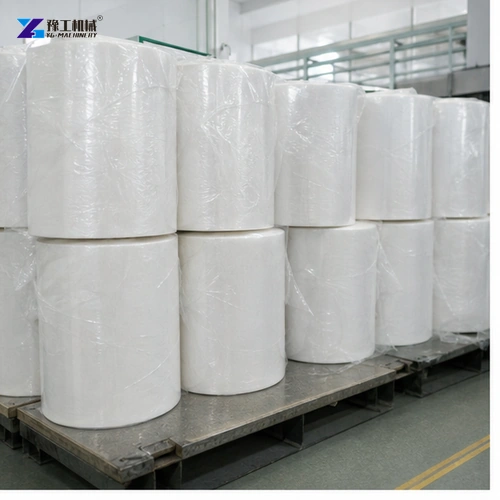
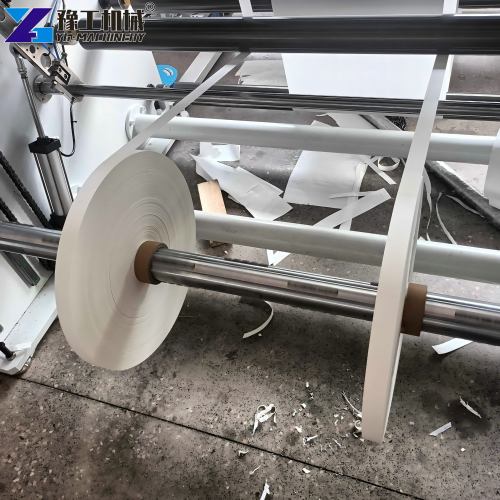
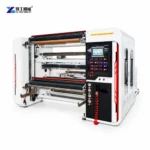
The unwind must protect a soft web from stretch and wandering
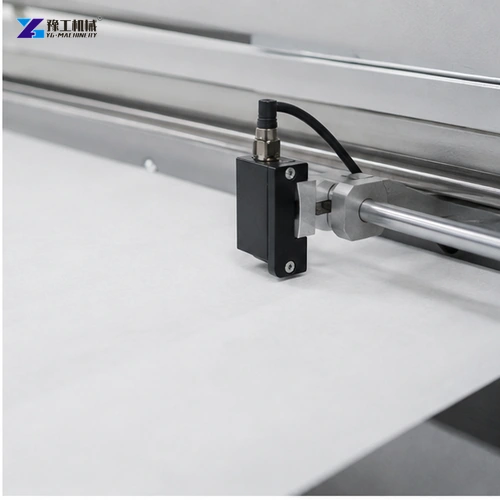
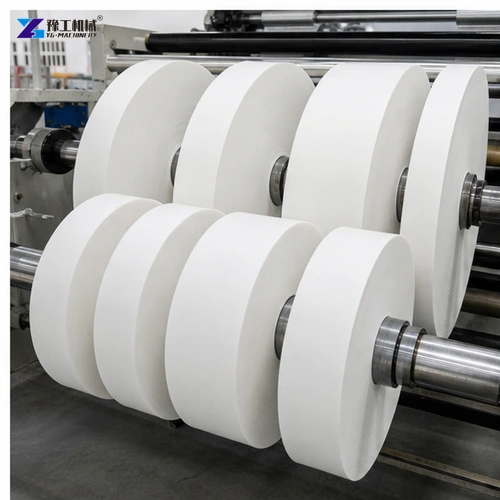
Edge guidance keeps the web referenced before the knife section
A non woven fabric slitting machine must do more than divide a wide roll into narrower widths. The web may be soft, extensible, porous or easily marked, and its behavior can change with basis weight, fiber bonding and winding tension. A machine that runs smoothly on dense paper may pull, curl or produce fuzzy edges when the same settings are applied to lightweight spunbond or meltblown material.
The purchasing task is therefore to match the web path, knife system and rewind control to the buyer’s actual material. Maximum speed and parent-roll size define only the outer machine envelope. Stable production depends on how the roll unwinds, how the edge is referenced, how tension changes through the slitting zone and how each finished roll is built. Representative trials are the safest way to convert a catalogue specification into a production decision.
What Material Data Should Be Confirmed Before Selection?
Send samples and a material schedule, not only a product name. State the nonwoven process, fiber composition, basis-weight range, thickness, usable width, surface treatment and whether the web stretches across or along the machine direction. Include the parent-roll diameter, core size, weight, splice condition and maximum telescoping already present when rolls reach the converter.
The finished-roll requirement is equally important. List every routine slit width, minimum width, number of lanes, core material, target diameter, roll hardness and permitted edge offset. Explain whether the roll goes to bag making, filtration, hygiene converting, lamination or another process. Downstream equipment may be less tolerant of loose winding, trapped air or edge variation than the slitter itself.
Dust, lint and electrostatic behavior should be reported from real production. These factors influence extraction, cleaning access, sensor reliability and operator safety. If an embossed or laminated web has a preferred face, mark the required winding direction. These details allow a non woven fabric slitting machine proposal to address the material route instead of treating every flexible web as paper.
Provide the parent roll, finished-roll schedule and representative samples. YG can compare the required envelope with the available machine range and identify the trials still needed.
How Should Tension And Web Guidance Be Controlled?
The unwind must deliver enough braking force to prevent overrun without stretching the material. Tension should remain stable as parent-roll diameter falls. A web that is already wrinkled or unevenly wound cannot be corrected by increasing tension; excessive force may narrow the web, deform the edge or make finished rolls recover after unloading.
Why Does The Unwind Need A Defined Operating Window?
Shaft type, chuck support, brake response and roll weight determine whether the parent roll can accelerate and stop safely. The supplier should know the heaviest roll and normal changeover method. Dancer or load-cell feedback may be considered where the material range demands tighter control, but the selection must be based on measured web behavior rather than the presence of an impressive control panel.
Where Should The Edge Guide Reference The Web?
The sensor should read a reliable edge or printed reference before the knife section, and the correction mechanism must move smoothly without hunting. Transparent, highly porous or irregular edges can require a suitable sensing method. Ask the trial team to record lateral movement at the unwind, immediately before slitting and at the rewind so the true source of width variation is not hidden.
An automatic slitting machine can repeat stored settings only when the material and setup are consistent.
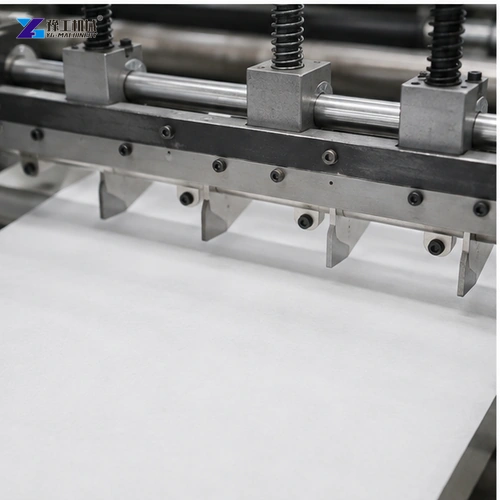
Knife choice depends on fiber structure and accepted edge condition
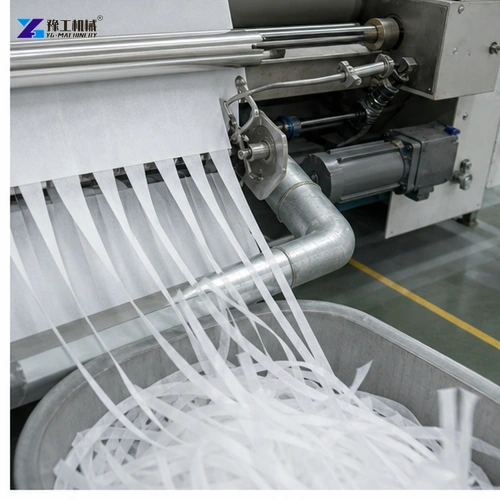
A production trial should expose linting, pulling and edge distortion
Which Knife System Produces The Required Nonwoven Edge?
Knife selection begins with the web construction and accepted edge, not with a generic claim that one method cuts every fabric. Shear, razor or crush arrangements act differently on bonded fibers, laminates and soft bulky webs. The cutting zone must support the material so the edge is separated cleanly instead of being drawn between blades.
Inspect both sides of the finished roll under downstream conditions. Look for lint, fused fibers, pulled strands, edge thickening, waviness and width drift. Unwind a trial roll, sample several positions and record the knife overlap, clearance, holder pressure and line tension that produced the accepted result.
Blade access also affects operating cost. Confirm how knives are positioned, guarded, cleaned and replaced; whether the setting scale is repeatable; and how long a normal width change requires. When many narrow lanes are needed, accumulated setup error and shaft deflection become more important than a single nominal minimum-slit figure.
Send the material sample and accepted edge standard so YG can plan a cutting trial around the actual fiber structure and slit widths.
Which Published Parameters Define The Machine Envelope?
The YG range below is published for roll slitting and provides a starting envelope for review. It should be verified against the actual nonwoven because the listed limits do not guarantee clean separation, stable tension or finished-roll quality for every fiber structure.
Published Parameter
YG-1300
YG-1600
YG-1800
Maximum Roll Width
1300 mm
1600 mm
1800 mm
Maximum Unwind Diameter
≤ φ1400 mm
≤ φ1400 mm
≤ φ1400 mm
Minimum Slitting Width
30 mm
30 mm
30 mm
Maximum Rewind Diameter
≤ φ1000 mm
≤ φ1000 mm
≤ φ1000 mm
Listed Running Speed
≤ 350 m/min
≤ 350 m/min
≤ 350 m/min
Total Power
24 kW
26 kW
30 kW
Power Supply
380 V / 50 Hz
380 V / 50 Hz
380 V / 50 Hz
Machine Weight
4000 kg
4500 kg
5500 kg
Overall Dimensions
3300 × 3150 × 1930 mm
3300 × 3450 × 1930 mm
3300 × 3650 × 1930 mm
Maximum width must include the usable material and any edge trim. The parent-roll diameter is useful only when core, weight and support method are also acceptable. Minimum slit width should be confirmed for the requested lane count and material, while the published speed is a mechanical upper limit rather than a promise of saleable output.
Compare utilities and floor layout as a complete system. A line may need loading equipment, trim handling, extraction, inspection space and finished-roll removal beyond the machine footprint. Voltage and frequency must be reconfirmed for the destination. Buyers comparing this range with a paper roll slitting machine should treat the table as an initial mechanical envelope and use trials to establish nonwoven performance.
Rewind control must manage width and tension across every lane
Accepted rolls should be firm, aligned and ready for downstream use
What Makes A Non Woven Fabric Slitting Machine Rewind Stable?
Finished rolls should have controlled hardness, aligned edges and sufficient stability for packing and downstream unwinding. That result depends on the relationship between slit width, shaft support, core quality, torque control and web tension. Narrow lanes can react differently across the same shaft, especially when the incoming gauge or tension is not uniform.
Specify whether differential shafts, individual friction elements or another rewind arrangement are required. The buyer should provide maximum finished-roll weight and explain how rolls will be removed without edge damage. Cores need the correct internal diameter, wall strength, width and squareness. A poor core can create vibration, eccentric winding and false conclusions about machine performance.
Trial acceptance should include a complete rewind, not a short strip. Measure width and edge alignment at several roll diameters, inspect the core area and outer wraps, then unwind enough material to reveal trapped wrinkles or tension recovery. Record speed changes during acceleration and deceleration. The result should be a repeatable recipe for the product family, not one attractive sample produced at an undisclosed low speed.
How Should Output And Changeover Be Compared?
Theoretical web speed does not equal shift output. Build a cycle that includes parent-roll loading, threading, knife positioning, core preparation, acceleration, production, deceleration, finished-roll removal, cleaning and inspection. Add realistic allowance for splices and roll changes. This exposes whether a faster line actually saves labor or merely moves the bottleneck to handling.
Product mix changes the answer. A converter running one width all day values sustained stability, while a short-run operation may gain more from quicker settings and accessible changeover. Ask suppliers to calculate output from the same roll schedule and acceptance criteria. The supporting slitting equipment, carts and lifting aids should be included in that comparison.
If production targets, staffing and changeover mix are available, YG can review the practical cycle instead of quoting output from headline speed alone.
Core setup and changeover time belong in the production calculation
Recorded trial settings make quotation promises measurable
What Evidence Should A Purchase Trial Record?
Use representative parent rolls, including a difficult but normal material. The trial record should state the web, roll condition, knife setup, tension settings, guide reference, running speed, lane widths, core specification and final diameters. Attach photographs and measurements of the finished edges and rewind build. Any manual intervention during the run should also be noted.
Define acceptance before the test. Useful criteria can include width tolerance, visible edge defects, telescoping, roll hardness, maximum waste, changeover time and saleable output over a full roll. Requirements must come from the buyer’s process; YG should not invent tolerances that the downstream line has not approved.
A complete quotation should separate the base machine, unwind and rewind configuration, knives, guiding, trim or dust handling, loading aids, electrical standard, spare parts, installation and commissioning. With the same scope and evidence, buyers can compare suppliers on the cost of accepted rolls rather than on an incomplete machine price.
No. Fiber bonding, basis weight, stretch, surface treatment and roll quality can require different tension and knife settings. Representative material trials are essential.
Does The Listed Speed Equal Production Speed?
No. Saleable speed depends on material stability, slit quality, rewind control, changeovers and inspection requirements.
How Is Minimum Slit Width Confirmed?
Confirm the complete lane arrangement, knife method, shaft support, core plan and web behavior during a full-width trial.
What Samples Should Be Sent To YG?
Send normal and difficult parent-roll samples, finished-roll requirements, rejected-edge examples and the downstream acceptance standard.
Should The Quotation Include Loading Equipment?
Yes, when roll weight or site handling requires it. Loading and unloading method affect safety, floor space and real cycle time.
Selecting a non woven fabric slitting machine is an exercise in controlled web conversion. The published width, diameter and speed figures define a useful starting range, while material trials prove whether tension, cutting and rewinding can produce acceptable rolls. A purchasing package built around real samples and measurable acceptance criteria gives the supplier enough evidence to configure the line responsibly.