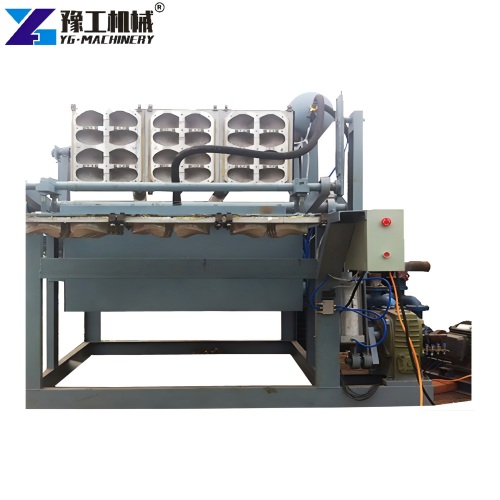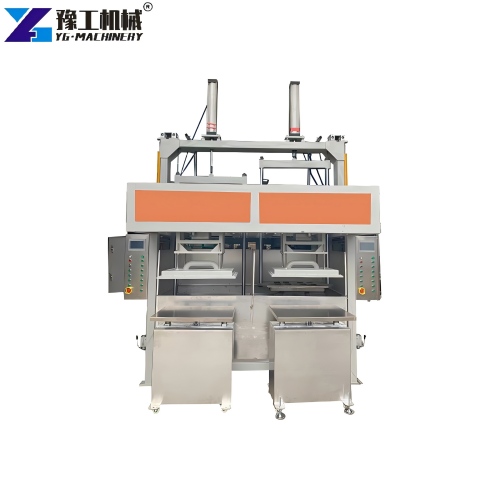
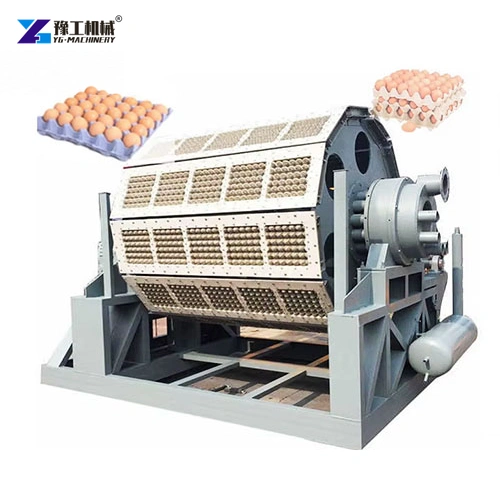
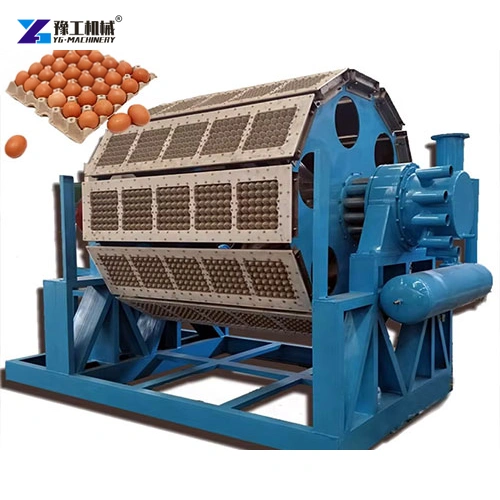
An egg tray molding machine converts prepared waste-paper pulp into wet molded-fibre trays. A forming mould takes up pulp from a controlled slurry, a vacuum step helps create the wet shape, and the newly formed blank transfers to the next stage for drying and stacking. The machine’s role is the forming part of a packaging line; it does not, by itself, turn loose waste paper into a finished dry tray ready for delivery.
YG lists the YG-1*3 through YG-6*8 configurations, with stated capacities from 1,000 to 7,000 pieces per hour. The model pattern is paired with a different mould count and installed power. Buyers should treat those values as the published configuration range and compare forming capacity with the drying and handling stages that determine finished, saleable output. See YG’s egg tray machine product page for the machine family.
What Does the Egg Tray Molding Machine Actually Do?
The forming station creates the tray geometry from prepared pulp. The pulp mixture is drawn against the mould surface, water is removed through the forming system, and the wet blank is released or transferred for drying. The mould shape determines the pockets, support ribs, edge profile and stack fit of the tray product.
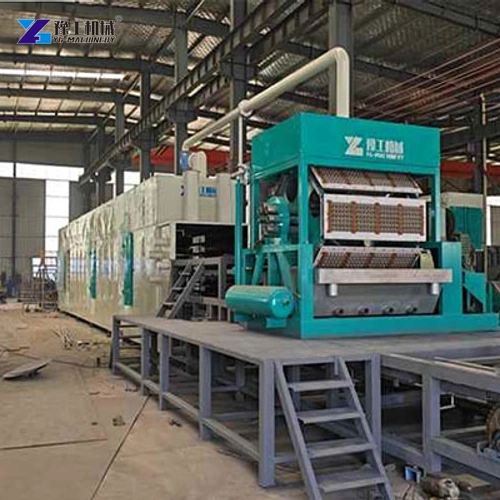
This distinguishes the forming machine from the full production line. Waste paper must be prepared into a usable pulp slurry, while wet trays need to be transferred and dried before they can be stacked or packed. A buyer comparing only the moulding station can miss the equipment and floor space needed before and after forming.
The actual output also depends on the chosen mould and the product format. A tray for a different egg count or protective geometry may need a different mould. Confirm the sample shape, dimensions and stacking behaviour before finalizing a mould specification; the hourly model rating does not mean every tray design will run at the same rate.
Which Businesses Use an Egg Tray Molding Machine?
Molded-fibre packaging manufacturers use egg trays to supply poultry farms, egg collection businesses, packers and distributors that need protective packaging for handling and transport. A paper-pulp packaging plant may make trays as one product among several molded-fibre items, provided the forming mould and downstream line are configured for each product.
A poultry operation with regular in-house packaging demand may evaluate production to secure a local supply, while a packaging converter may run the equipment as a product line for multiple customers. Those are different operating cases. A converter needs repeatable mould changes and order scheduling; an integrated egg business needs the packaging format, production volume and delivery rhythm to match its own grading and packing operation.
The machine is most relevant where the buyer can organize a consistent pulp feed, keep the moulding station supplied and dry the wet blanks at the required pace. A small workshop without space for pulp preparation and drying may find that the forming machine itself is not the limiting investment; the rest of the line may control practical output.
- Molded-pulp packaging manufacturers producing egg trays for multiple buyers.
- Egg packers or poultry businesses evaluating in-house tray supply for a defined demand.
- Packaging plants using interchangeable moulds for related pulp-molded products, where the selected machine supports that format.
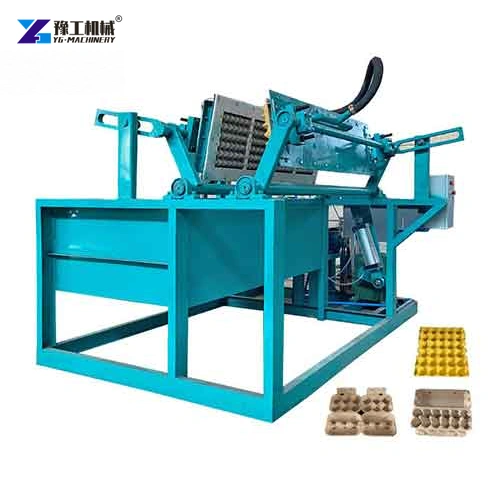
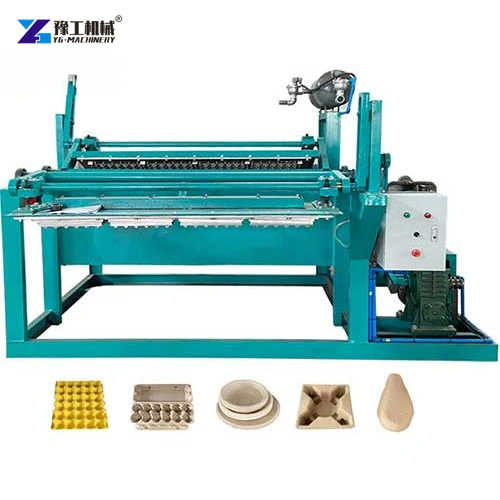
YG Egg Tray Molding Machine Models and Listed Capacity
Each model below is shown with the manufacturer’s mould count, listed forming capacity, installed power and worker range. Preserve the model notation exactly; the asterisk-separated model name is not a multiplier to reinterpret as a guaranteed hourly production calculation.
| Model | Capacity (pcs/h) | Moulds | Power | Workers |
| YG-1*3 | 1,000 | 3 | 40 kW | 3–5 |
| YG-1*4 | 1,500 | 4 | 40 kW | 4–6 |
| YG-3*4 | 2,500 | 12 | 50 kW | 4–6 |
| YG-4*4 | 3,500 | 16 | 60 kW | 4–6 |
| YG-4*8 | 4,500 | 32 | 130 kW | 4–6 |
| YG-5*8 | 5,500 | 40 | 140 kW | 5–7 |
| YG-6*8 | 7,000 | 48 | 186 kW | 6–8 |
The page separately lists electricity consumption as 28, 29, 35, 42, 91, 98 and 130 kW/h for these configurations. The unit is reproduced as printed; request confirmation of the intended consumption unit and measurement basis before preparing an energy-cost estimate. Installed power and energy consumption are not interchangeable figures.
The capacity values refer to the stated machine configuration, not automatically to finished dried trays packed per hour. Drying time, moisture removal, tray geometry, mould cycle, stoppages and downstream stacking can reduce saleable throughput. A line proposal should explain whether the stated capacity is at the forming station or at final dry-product discharge.
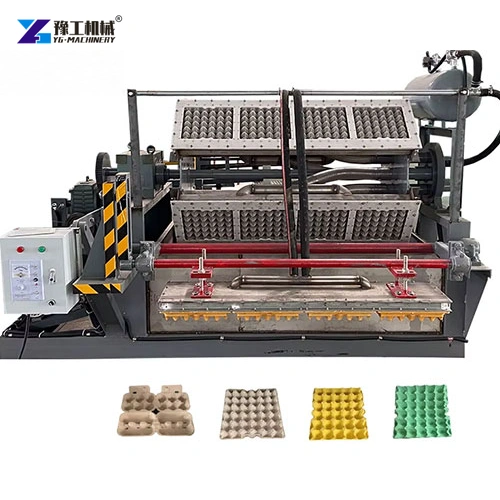
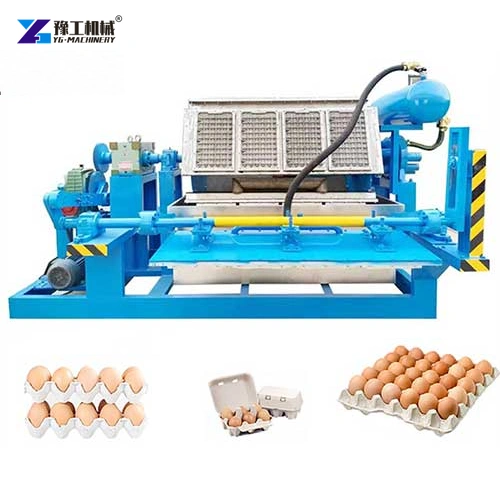
Follow the Tray From Pulp Preparation to Dry Stacking
Start with waste paper sorting and pulping so contaminants and oversized pieces do not travel into the forming system. Screening and slurry preparation help maintain consistent fibre condition. If feed concentration varies widely, mould filling and release may become less repeatable, affecting tray shape and wet-blank handling.
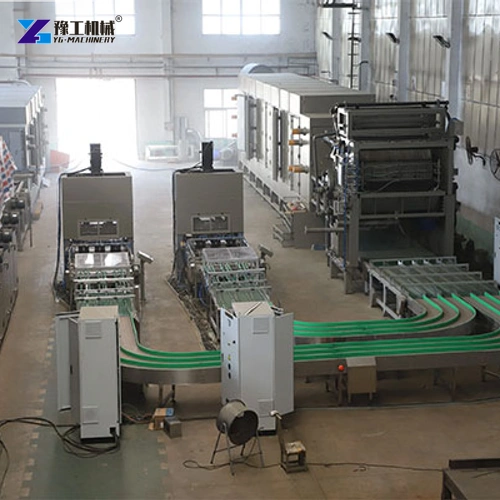
At the forming stage, the mould creates the specified tray geometry. The wet blank then transfers to a drying stage. The dryer must accept the same hourly flow that the forming machine produces; otherwise trays accumulate between stages or the moulding equipment must wait. Stacking and packing add another capacity boundary after drying.
This is why production planning should compare the whole sequence rather than multiply a mould count by an assumed cycle. Review how the line handles wet transfer, drying capacity, recirculation, dry-tray collection and mould changeover. A well-matched line aims for stable flow and a tray that meets the buyer’s fit and protection requirement, not just a high nominal forming figure.
If you are comparing line sizes, share the target tray format, expected shifts and available drying arrangement so the model rating can be considered within the full process.
Egg Tray Molding Machine FAQs
No. It forms wet pulp trays. Pulp preparation comes before molding, and wet blanks need drying and downstream stacking or packing before they are finished products.
The listed configurations are YG-1*3, YG-1*4, YG-3*4, YG-4*4, YG-4*8, YG-5*8 and YG-6*8, with stated capacities from 1,000 to 7,000 pcs/h.
Not necessarily. The published figure is tied to the listed machine configuration. Drying, tray design, stoppages, transfer and stacking affect the number of finished trays available for packing.
Molded-pulp packaging manufacturers, egg packers and poultry businesses with defined tray demand may consider one. Their line needs differ: a converter may prioritize order flexibility, while an integrated packer may prioritize matching production to its own packing schedule.
Installed power is the equipment power rating. The page separately lists electricity consumption in kW/h; because that printed unit and measurement basis need confirmation, ask the supplier before estimating energy cost.
Choose a Forming Model That Fits the Entire Line
The right egg tray molding machine is the configuration that makes the required tray format at a rate the pulp-preparation, drying and handling stages can support. Use YG’s model-specific mould count and output data to shortlist the forming station, then verify how the quoted line turns wet blanks into accepted dry trays.
For a model comparison, include the tray format, target output, drying method, operating shifts and available floor space.