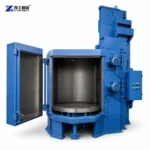

Ordering wear items from appearance alone can stop a factory line twice: first when the original component fails and again when the replacement does not fit. Shot blasting machine spare parts should be identified from the machine model, installed assembly, dimensions, orientation and operating symptom. A blast wheel component that looks similar may still differ in balance, mounting, material or directional geometry.
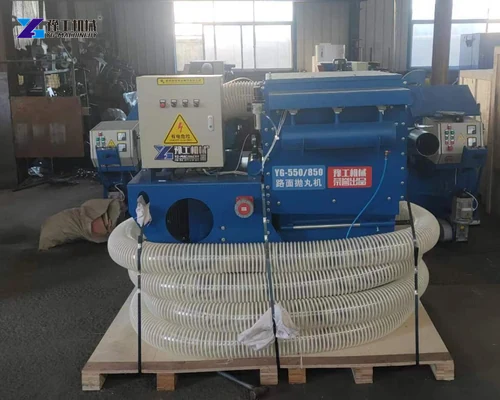
This guide uses documented YG floor-shot-blaster components to explain a repeatable parts request. The YG-550 manual identifies the blast wheel, directional sleeve and top, centre and side liners as wear items. Those references remain model-specific; roller-conveyor, hanger and tumble-belt machines need their own drawings, serial data and service limits.
Confirm the installed family on the industrial shot blasting machine page and use the shot blasting machine maintenance guide to connect parts stocking with inspection intervals.
Identify Shot Blasting Machine Spare Parts by Model
Start with a clear nameplate photograph, machine model, serial information where available and the working width or chamber size. Add one wide photograph that shows where the part sits and close photographs of both faces, mounting holes and nearby components. Record quantities and whether left- and right-hand versions exist.
Do not remove a component only to obtain a photograph until the machine is isolated under the site’s lockout procedure. Mark the installed orientation before disassembly. If the nameplate is damaged, provide the original order reference, motor data, overall machine view and measured mounting pattern so the supplier can narrow the correct shot blasting machine spare parts drawing.
Send the main project dimensions and material requirement for a model review.
REVIEW MY PROJECT REQUIREMENTS


Match Blast Wheel and Directional Control Parts
The blast wheel accelerates abrasive at high speed, so blades, impeller, control cage or directional sleeve and related fasteners must belong to the approved assembly. Uneven wear or a mixed set can create vibration and move the blast pattern. Replace high-speed parts according to the manufacturer procedure rather than welding a worn wheel component.
The YG-550 instructions require the directional sleeve to be adjusted after blast-component replacement. That does not create a universal position for every model. Confirm rotation direction, preserve the documented assembly order and use a controlled test surface to verify the pattern before returning to production.
Inspect Liners, Seals and Housing Protection
Liners protect the machine structure from direct abrasive impact. Compare plate outline, thickness, hole spacing, curvature and material with the removed component. Replace a liner before a hole exposes the housing. Inspect the adjacent fasteners and backing surface because a correct new plate cannot repair an already distorted mounting area.
Seals, curtains, floor magnets and door strips control abrasive escape for different machine types. A parts request should state the opening dimensions, seal position and observed leakage. Do not select a seal only by length; profile, thickness, overlap and fastening method determine whether it contains media without interfering with the workpiece.
| Part group | Evidence to provide | Reason for checking |
| Blast wheel assembly | Model, rotation, installed photos and part markings | Balance and geometry are assembly-specific |
| Directional sleeve or control cage | Orientation, opening and matching wheel model | Incorrect position changes the blast pattern |
| Liners | Outline, thickness, holes, curvature and location | Similar plates may not protect the same surface |
| Seals and curtains | Profile, dimensions, overlap and fixing method | Controls abrasive leakage around openings |
| Recovery parts | Elevator, screen, valve or hose model and symptom | Flow faults may originate elsewhere in the circuit |
| Dust-control parts | Collector model, filter or hose dimensions | Airflow and fit must match the installed system |
| Electrical items | Label, voltage, terminals and qualified diagnosis | Avoids unsafe or incompatible substitution |


Include Recovery and Dust-Control Spare Parts
A stable blast circuit also depends on hoses, screens, bucket-elevator parts, separator elements, filters and valves. Identify the symptom as well as the component: low media level, carryover, dust escape, restricted suction or irregular flow. This helps separate a worn part from an upstream blockage or operating issue.
For hoses and filters, send dimensions, connection type, material condition and collector model. Electrical items require photographs of the label, voltage and terminal arrangement, but diagnosis and replacement belong to qualified personnel. Never bypass an interlock or substitute an unverified control component to keep production running.
Build a Shot Blasting Machine Spare Parts Stock List
Rank shot blasting machine spare parts inventory by wear rate, delivery time and shutdown consequence. Frequently inspected liners, seals and selected wheel components may justify local stock, while large structural items can remain order-on-demand. Use operating hours and measured condition to set reorder points instead of copying a generic list from another machine.
Store balanced or matched parts as complete sets when required, label them by machine and protect machined faces from corrosion or impact. Keep the supplier drawing, receipt date and installation record with the stock item. After replacement, record the removed condition and hours so future quantities are based on actual factory use.
Share the intended equipment scope so YG can check the configuration and included accessories.

Send a Complete Shot Blasting Parts Inquiry
A useful inquiry contains the machine type, model, serial data, workpiece, abrasive, operating hours, symptom, required quantity, destination and photographs with measurements. State whether the request is for an urgent repair, planned shutdown or initial stock. Ask the supplier to identify parts that must be replaced together.
Request a quotation that lists part name, applicable model, drawing or reference number, quantity, included fasteners, packing and lead time. Confirm all dimensions against the installed machine before shipment. This evidence-led approach makes shot blasting machine spare parts easier to compare and reduces incorrect substitutions.
Provide the final site and delivery details when you are ready for a complete quotation.

Shot Blasting Machine Spare Parts FAQ for Factory Maintenance
Send the nameplate, model, serial information, part location, photographs, dimensions, quantity and operating symptom.
No. High-speed components must match the approved assembly, balance and installation procedure.
Follow the model limit and replace it before wear exposes or damages the protected housing.
Prioritize by observed wear, delivery time and shutdown consequence rather than buying a generic list.