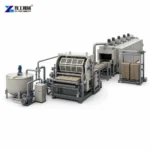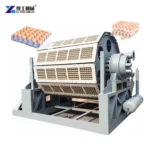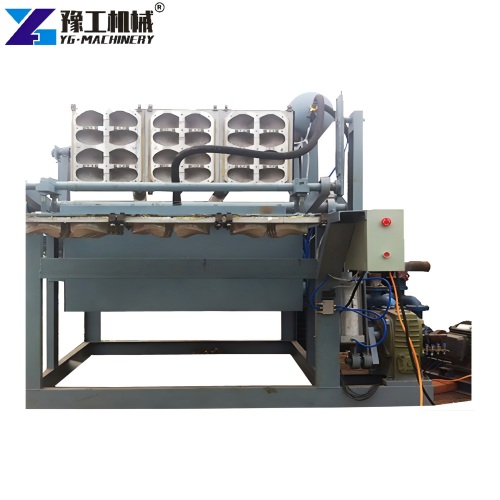

An egg tray factory is only as fast as its slowest stage. A forming machine rated at 7000 trays per hour cannot deliver that saleable output if pulp preparation fluctuates, wet trays wait for drying space, molds are changed too often or packing cannot clear finished products. Buyers should therefore define the required packed-tray output and work backward through pulp, forming, drying and handling. This guide explains how to balance those stages before choosing equipment.
How Many Saleable Egg Trays Must The Factory Produce?
Start with customer orders, tray design and operating schedule rather than the largest catalog number. Convert monthly demand into trays per effective production hour after allowing for shifts, cleaning, mold changes, maintenance and normal stoppages. Distinguish formed pieces from accepted, dry and packed trays. This prevents the factory plan from assuming that every forming cycle becomes a shipped product.
Tray weight and cavity count also matter. A heavier tray consumes more pulp and drying energy, while a different mold arrangement changes pieces per cycle. Define egg size, tray dimensions, stacking requirement and strength target before comparing hourly capacity. Sample approval should happen early because material recipe and geometry influence every downstream stage.


Can Pulp Preparation Feed The Forming Machine Consistently?
Waste paper must be sorted, pulped, screened and diluted to a controlled consistency. Contamination causes blocked lines, damaged molds and weak tray areas. An undersized pulper or storage tank forces the forming section to wait; an unstable mixture produces variable wet weight and drying time. The pulp system should maintain enough prepared stock for normal operation while allowing the recipe to be corrected without stopping the entire line.
Ask what paper grades are locally available and whether printed, coated or heavily contaminated material will enter the furnish. Record water quality and the plan for process-water reuse. Pump capacity, tank volume, agitation and pipeline arrangement should be sized around the selected forming rate and factory layout, not copied from another plant with different raw material.
Send YG the available paper types, tray weight and target output to review the pulp and forming balance.


Is Drying The Real Capacity Limit?
Wet trays leave the molds with most of the water still to be removed. Natural drying needs land, racks, handling labor and suitable weather; it may suit smaller production where climate and space are favorable. Brick or metal drying lines provide more controlled throughput but require fuel, airflow design and heat management. The dryer must accept the actual wet-tray rate without creating a queue that deforms trays or slows the forming machine.
Evaluate drying by accepted trays per hour, energy source, local fuel cost, moisture target and seasonal conditions. Confirm how trays transfer from forming to drying and from drying to stacking. A fast dryer does not solve uneven wet weight, and a large forming section cannot compensate for limited drying residence time. The two stages must be commissioned together.

How Do Molds, Labor And Packing Affect Output?
Mold quantity determines how many pieces are formed per cycle, but mold quality and vacuum distribution determine whether those pieces release cleanly. If the factory will produce several tray sizes, include changeover time, mold storage and sample approval in the plan. Operators need safe access for cleaning blocked holes and inspecting worn surfaces without disturbing alignment.
Labor should be mapped by station: pulp preparation, forming supervision, drying transfer, quality inspection, stacking, packing and maintenance. Automatic transfer can reduce manual handling, but it also increases the need for coordinated sensors and maintenance. Finished trays require time to cool and stabilize before compression or bundling. Packing capacity and warehouse space should match peak accepted output.
| Model | Capacity | Forming Molds | Total Power | Electricity Use | Workers |
| YG-1×3 | 1000 pcs/h | 3 | 40 kW | 28 kWh | 3–5 |
| YG-1×4 | 1500 pcs/h | 4 | 40 kW | 29 kWh | 4–6 |
| YG-3×4 | 2500 pcs/h | 12 | 50 kW | 35 kWh | 4–6 |
| YG-4×4 | 3500 pcs/h | 16 | 60 kW | 42 kWh | 4–6 |
| YG-4×8 | 4500 pcs/h | 32 | 130 kW | 91 kWh | 4–6 |
| YG-5×8 | 5500 pcs/h | 40 | 140 kW | 98 kWh | 5–7 |
| YG-6×8 | 7000 pcs/h | 48 | 186 kW | 130 kWh | 6–8 |


Which Utilities And Factory Areas Must Be Confirmed?
Prepare a layout showing raw-paper receiving, pulp preparation, forming, drying, packing, finished storage and maintenance access. Confirm electrical voltage and frequency, installed power, water source, drainage, dryer fuel, ventilation and compressed air where required. Floor loading, door size and internal transport routes should be checked before shipment. Space around tanks, pumps and molds is necessary for safe service rather than optional empty floor.
The table provides published reference figures, but final consumption depends on the selected drying method and auxiliary equipment. Obtain a scope list that separates supplied machinery from civil work, local piping, wiring, fuel system, installation labor and commissioning support. This makes quotations comparable and prevents a low machine price from hiding an incomplete plant budget.
Compare the YG egg tray manufacturing machine, egg tray production line and egg tray plant cost guide when planning equipment and total project scope.
Egg Tray Manufacturing Machine FAQ
Choose from realistic packed-tray demand, working hours, drying capacity, utilities and labor. Leave room for maintenance and normal stoppages.
Different approved molds can produce different formats when the forming range supports them. Confirm dimensions, cavity count and changeover procedure.
Natural drying suits lower output where land and weather are favorable. Controlled drying supports steadier production but needs fuel, airflow and capital planning.
Common waste-paper grades can be used after sorting and pulping. Provide local paper samples or descriptions so the recipe and cleaning needs can be reviewed.
Provide tray design, required packed output, paper source, drying preference, voltage, fuel, water, factory dimensions, destination and automation expectations.
Build The Quote Around A Balanced Production Line
Define the saleable output, approved tray, raw-paper supply and drying method first. Then verify pulp storage, forming capacity, transfer, packing, utilities and staffing. YG can use that information to prepare a line configuration and quotation that protects usable factory output instead of oversizing one machine.